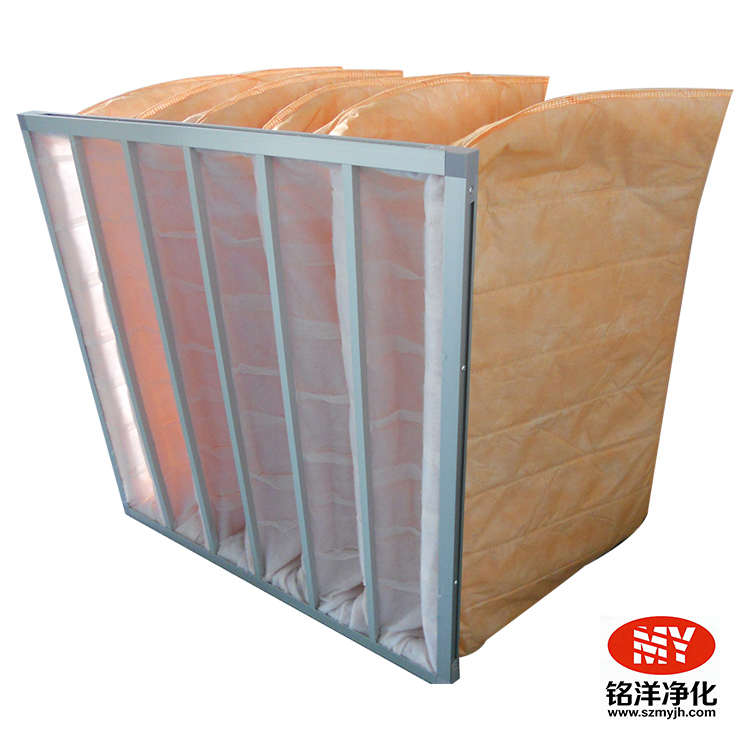
Conclusion first: Distinguish between frame gap sealing gasket compression and rail deformation issues. For a “medium-efficiency filter frame sealing not tight” condition, the most prudent approach is to first confirm the installation location, project documentation, and on-site data, then make a judgment under comparable operating conditions; do not draw conclusions based solely on product names, a single number, or a fixed date.
1. Clarify the applicable boundaries first
The goal of maintenance is not to replace parts mechanically on a calendar basis, but to timely detect abnormalities under comparable operating conditions, perform standardized disposition, and retain traceable records.
On-site work for a “medium-efficiency filter frame sealing not tight” condition should follow the sequence: assess first, then act, and finally verify. Balance differential pressure, dust-holding capacity, and protection of the downstream HEPA filter or HEPA section. Do not omit inspection of bag-type or filter element condition, frame sealing, compression state, differential pressure trend, rated airflow, and upstream operating condition; treating medium-efficiency filters as freely washable or ignoring bypass leakage weakens protection of downstream filtration.
In any intermediate filtering section of an air handling unit and protection sections before HEPA sections, product parameters must be understood together with actual installation location, system airflow, upstream/downstream conditions, and on-site management requirements. Especially when involving controlled environments, continuous operation, or change management, use this article as a communication and inspection framework, then determine final actions based on approved project documents, equipment data, and on-site measurements.
2. What information should you check on-site?
| Inspection dimension | Items to verify | Common misconceptions |
|---|---|---|
| Specifications and site conditions | Confirm dimensions, rated airflow, efficiency or functional requirements, mounting structure, and maintenance accessibility. | Avoid treating similarly named or dimensionally identical products as directly interchangeable. |
| Operating data | Record baseline condition and observe differential pressure, airflow, equipment operation, or area condition under comparable operating points. | A single reading should not be interpreted without considering fan speed, valve positions, and upstream load. |
| Installation and sealing | Check orientation, positioning, compression, sealing elements, and frame/rail condition. | Differentiate between problems in the filter media itself and bypass leakage. |
| Maintenance closed-loop | Retain records of inspection, disposition, replacement, and necessary retests. | Before declaring an abnormality closed, confirm the system has been restored to the project-required state. |
From a data management perspective, initial values and trends are more valuable than a single “high” or “low” reading. Any abnormal reading should be rechecked under the same or comparable operating conditions — for example fan frequency, valve positions, operating time, upstream filter condition, and instrument tapping conditions. Only then can maintenance personnel distinguish real load changes from measurement or system condition variations.
3. Recommended inspection and disposition workflow
Confirm boundaries. First review project documents, equipment manuals, and on-site maintenance procedures to clarify the purpose, allowable conditions, and safety requirements for this inspection or work.
Collect baseline. Record bag-type or filter element condition, frame sealing, compression state, differential pressure trend, rated airflow, and upstream operating condition; if no historical baseline exists, establish an initial comparable data set.
Layered verification. Verify sequentially from the upstream environment, equipment condition, filter or component appearance, installation sealing to downstream performance—do not skip basic conditions and jump to conclusions.
Perform disposition. When replacement or adjustment is required, verify product specifications and installation orientation, and control risks of contamination, mechanical stress, and debris during disassembly and assembly.
Restore and record. After completion, check system restoration status; in scenarios requiring verification, arrange airflow, integrity/leak test, or environmental performance rechecks per project documentation.
For products that require replacement, verify model, dimensions, rated airflow, filtration class or function, frame and sealing method before disassembly. For non-standard requirements, supplement with installation drawings, rail or compression method, equipment position, and maintenance clearance information. Installation completion does not equal task completion — post-restoration data verification, cleaning of the work area, and record keeping are essential parts of the maintenance closed-loop.
4. How this links to related products or solutions
This topic can be considered alongside existing box-type medium-efficiency filter and F5 bag-type medium-efficiency filter. Pre-filters, intermediate filters, terminal filters, or clean equipment each play different roles; when selecting, modifying, or confirming non-standard sizes, organize site parameters and consult technical personnel. Technical advice should be based on actual operating conditions, not as a substitute for on-site confirmation.
5. Frequently asked questions
What maintenance records should be kept at a minimum?
It is recommended to retain the equipment or installation location, product model and batch, dimensions and rated parameters, installation date, initial pressure drop, inspection readings, abnormal dispositions, replacement personnel, and necessary retest results to form a traceable closed-loop.
Can I handle this solely on a fixed schedule?
Not recommended. Combine project documents, equipment manuals, differential pressure trends, airflow or environmental capability, installation state, and abnormal events to make decisions; fixed intervals should only be used as triggers for planned inspections and cannot replace on-site confirmation.
Must I replace the filter immediately upon detecting an abnormality?
First confirm the nature and risk level of the abnormality. For cases involving damage, moisture, obvious bypass leakage, or possible impact to a controlled environment, follow on-site procedures to isolate and organize an assessment; for anomalous readings, also verify instruments, fan, valves, and upstream/downstream filter status.
6. Conclusion
The essence of "How to handle a medium-efficiency filter frame that is not sealed tightly? Leak localization and rectification key points" is not to find a scenario-free standard answer, but to establish a repeatable, data-traceable, and closed-loop judgment method. Inspect around bag-type or filter element condition, frame sealing, compression state, differential pressure trend, rated airflow, and upstream operating condition, and link technical specifications, site status, and maintenance records to provide more reliable support for stable system operation.
References and scope of use
This article is intended for technical communication and maintenance planning of air filters and clean equipment and does not replace project design documents, equipment manuals, on-site risk assessments, or applicable regulations and quality system requirements. Cleanroom cleanliness classifications may refer to ISO 14644-1 (https://www.iso.org/standard/53394.html); HEPA filter product testing and performance documentation can be cross-checked with EN 1822 / ISO 29463 related guidance (https://www.camfil.com/en-us/insights/standard-and-regulations/en-1822-and-iso-29463-hepa-filter-factory-test).