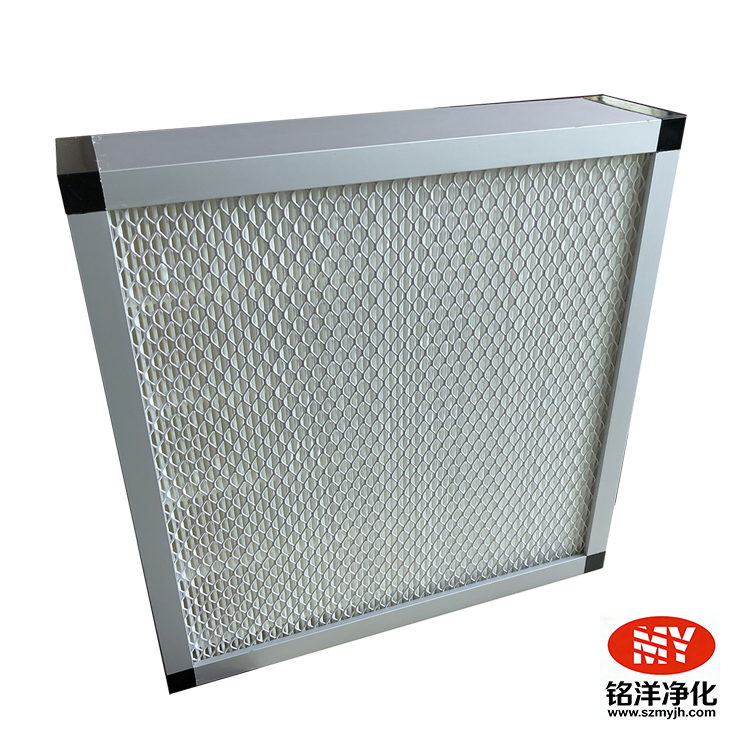
Conclusion first: Separate the description of temperature variation, sealed structures, and pre-use verification. For "high-temperature HEPA filter usage precautions," the safest approach is to first confirm the installation location, project documents, and on-site data, then make a judgment under comparable operating conditions; do not draw conclusions based only on the product name, a single number, or a fixed date.
1. Clarify the applicable boundaries of the issue
The goal of maintenance is not to mechanically replace parts on a calendar schedule, but to detect anomalies in comparable operating conditions in time, carry out standardized handling, and keep traceable records.
On-site work for "high-temperature HEPA filter usage precautions" should follow the sequence of assess first, then act, and finally verify. Manage filtration efficiency, system resistance, installation sealing and on-site verification as an integrated process. Do not overlook product labels and documentation, frames and seals, installation clamping, differential pressure trends, airflow, and retest results against project requirements; replacing based only on a fixed date or a single differential pressure value may miss risks caused by installation bypass leakage, system imbalance, and contamination events.
In any cleanroom terminal, HEPA supply outlet, fan filter unit (FFU), or high-grade air handling section, product parameters must be understood together with the actual installation location, system airflow, upstream and downstream conditions, and on-site management requirements. Especially for controlled environments, continuous operation, or change-management scenarios, use this document as a communication and inspection framework, then determine final actions based on approved project documents, equipment data, and field measurements.
2. What information should be checked on site?
| Inspection dimension | Items to verify | Common misconceptions |
|---|---|---|
| Specifications and site conditions | Confirm dimensions, rated airflow, efficiency or functional requirements, mounting structure, and maintenance accessibility. | Avoid assuming similarly named or dimensionally identical products are direct substitutes. |
| Operating data | Record initial conditions and observe differential pressure, airflow, equipment operation, or area status under comparable operating conditions. | A single reading should not be interpreted without considering fan frequency, valve positions, and upstream load. |
| Installation and sealing | Check orientation, positioning, clamping, sealing elements, and the condition of frames/tracks. | Distinguish problems with the filter media itself from bypass leakage of unfiltered airflow. |
| Maintenance closed-loop | Keep records of inspections, actions, replacements, and any required retesting. | Before declaring an anomaly closed, confirm the system has been restored to the project-required state. |
From a data-management perspective, baseline values and trends are more valuable than a single "high" or "low" reading. Any anomalous reading should be rechecked under the same or comparable operating conditions—for example, fan frequency, valve positions, operating period, upstream filter status, and instrument tapping conditions. Only then can maintenance personnel distinguish real load changes from measurement or system-condition variations.
3. Recommended inspection and disposition workflow
Define the boundaries. First review project documents, equipment manuals, and on-site maintenance procedures to clarify the purpose of this check or task, allowable operating conditions, and safety requirements.
Collect a baseline. Record the product label and documentation, frame and seals, installation clamping, differential pressure trends, airflow, and retest results against project requirements; if no historical baseline exists, establish comparable initial data first.
Layered verification. Verify items sequentially from upstream environment, equipment condition, filter or component appearance, installation sealing, to downstream performance—avoid skipping basic conditions and jumping to conclusions.
Execute disposition. If replacement or adjustment is required, verify product specifications and installation orientation, and control contamination, mechanical stress, and residual debris risk during disassembly and assembly.
Restore and record. After completion, check system recovery status; in scenarios that require verification, arrange corresponding airflow, integrity/leak test, or environmental performance retesting as specified in project documents.
For products that need replacement, verify model, size, rated airflow, filtration class or function, outer frame, and sealing method before disassembly. For nonstandard requirements, supplement with installation drawings, tracks or clamping methods, equipment location, and maintenance access information. Installation completion does not equal task completion—the closed-loop requires post-installation data verification, cleanup, and recordkeeping.
4. How to interface with related products or solutions?
This topic can be understood in connection with the existing high-temperature HEPA filter. Upstream filters, medium-efficiency filters, terminal filters, or clean equipment each play different roles; when selecting, modifying, or confirming nonstandard sizes, it is recommended to organize on-site parameters and consult technical personnel. Technical advice should be based on real operating conditions, not as a substitute for on-site confirmation.
5. Frequently asked questions
Can I act solely on a fixed cycle?
Not recommended. Combine project documents, equipment manuals, differential pressure trends, airflow or environmental capability, installation status, and abnormal events to form a judgment; a fixed cycle can serve as a trigger for planned inspection but cannot replace on-site verification.
If an anomaly occurs, must the filter be replaced immediately?
First determine the nature and risk level of the anomaly. For conditions involving damage, moisture exposure, obvious bypass leakage, or potential impact on the controlled environment, isolate per on-site procedures and organize an assessment; for anomalous readings, also verify instruments, fans, valves, and upstream/downstream filter status.
What maintenance records should be retained at minimum?
It is recommended to retain equipment or installation location, product model and lot, size and rated parameters, installation date, initial pressure drop, inspection readings, anomaly dispositions, personnel performing replacements, and any required retest results to form a traceable closed-loop.
6. Conclusion
The core of "Why confirm process temperature before using high-temperature HEPA filters? Thermal deformation and sealing risk" is not to find a one-size-fits-all answer detached from context, but to establish a repeatable judgment method with traceable data and closed-loop handling for anomalies. Verify product label and documentation, frame and seals, installation clamping, differential pressure trends, airflow, and retest results against project requirements, and connect technical specifications, site conditions, and maintenance records to provide more reliable support for stable system operation.
References and scope of use
This document is intended for technical communication and maintenance planning of air filters and clean equipment and does not replace project design documents, equipment manuals, on-site risk assessments, or applicable regulations and quality system requirements. Cleanroom air cleanliness classification ranges may be referenced from ISO 14644-1; product testing and performance information for HEPA filters can be cross-checked with EN 1822 / ISO 29463 related guidance.